Top 5 Flare System Configurations for LNG Terminals: A 2026 Recommendation List
LNG receiving terminals and natural gas processing facilities do not flare the way a refinery does. Relief loads arrive quickly, the gas is cold, and the flare plot usually sits inside a dense layout next to storage tanks, loading arms and bunkering berths, where radiation, noise and stack height are constrained by neighbouring assets. This recommendation list ranks the five Zexuan flare system configurations that fit LNG-terminal duty most directly in 2026: the ZX-SMF Series skid-mounted LNG/LPG and BOG flare system, the ZX-EGF Series enclosed ground flare, and three elevated configurations — the ZX-GWF Series guyed-wire flare, the ZX-SSEF Series self-supported flare, and the ZX-DSF Series derrick-supported flare with a demountable option.
The order below is a duty-fit ranking, not a claim about brand superiority. Each position is decided by documented design characteristics: cryogenic compatibility, skid-mounted mobility, combustion efficiency, radiation and noise control, turndown, structural footprint, and the speed at which a unit can be installed and commissioned. Where a configuration has a real limitation, the limitation is stated, because a selection list that hides trade-offs cannot be used at the evaluation stage.
Ranked at a glance
- #1 ZX-SMF Series — skid-mounted LNG/LPG and BOG flare, cryogenic service compatible, fast installation and commissioning. Best overall fit for LNG receiving terminals and bunkering.
- #2 ZX-EGF Series — enclosed ground flare, combustion efficiency up to 99.9%, low radiation and low noise design, suited to space-limited sites.
- #3 ZX-GWF Series — guyed-wire elevated flare for high-volume emergency relief; a reference installation uses a 60 m structure with a DN350 flare tip.
- #4 ZX-SSEF Series — self-supported elevated flare for sites where guy-wire anchor areas are not available.
- #5 ZX-DSF Series — derrick-supported elevated flare with demountable option for heavy-duty stacks and difficult sites.
Why LNG Terminals Need Their Own Flare Configuration Logic
Flare systems for LNG terminals and gas processing facilities are selected against a different set of constraints than refinery relief systems, and the differences are technical rather than commercial.
Cryogenic service. LNG, LPG and boil-off gas (BOG) streams can reach the flare header at low temperature, so material selection has to account for low-temperature service. Zexuan's ZX-SMF Series is specified as cryogenic service compatible and is built with carbon steel, SS304, SS316L and low-temperature materials for LNG service. A configuration that is only validated for ambient hydrocarbon gas is not interchangeable with one that is specified for cryogenic duty.
Emergency release conditions. Terminal relief events are short, high-rate and non-negotiable in terms of response. Two design parameters matter most here: turndown capability, which for Zexuan elevated flares reaches up to 100:1, and combustion efficiency, which is typically ≥98%–99.9% for elevated flares depending on design and operating conditions and up to 99.9% for the ZX-EGF enclosed ground flare.
Plot space and neighbourhood exposure. Terminals are compact. Enclosed ground flares are designed for limited-space areas with low radiation and low noise output, which matters when the flare is sited near tank bunds, control rooms or jetty access roads. Elevated flares solve the same problem by distance instead of enclosure, using stack height of 10 m to 150 m+ to place the flame away from grade-level exposure.
Deployment speed. Terminal expansions, bunkering additions and BOG-handling upgrades often have to be executed during short shutdown windows. A compact skid-mounted design with fast installation and commissioning can be integrated without a long structural construction programme on site.
Market and Regulatory Context for 2026
Three published data points frame why flare configuration decisions are being revisited across the LNG and gas-processing sector in 2026.
- Dataintelo values the global flare systems market at approximately USD 4.8 billion in 2025, driven by regulatory pressure on hydrocarbon emissions and recovery in oil and gas investment.
- The World Bank reported global gas flaring volumes of 151 billion cubic meters (bcm) in 2024, the highest level since 2007 — a reminder that flare hardware is still the primary safety barrier on most hydrocarbon sites.
- Intel Market Research values the global totally enclosed ground flare segment at USD 113 million in 2024, with growth linked to destruction efficiencies exceeding 98%.
On the regulatory side, flare system design is primarily governed by API Standard 521 (Pressure-Relieving and Depressuring Systems), which among other requirements specifies a minimum flare header slope of 1/4 inch per 10 feet for drainage. That single requirement explains why configuration choices cannot be made after layout: header routing, knockout drum position and flare type are linked from the first design iteration.
Regionally, Grand View Research puts Asia-Pacific at a 35% share of the flare gas recovery system market as of 2025, the largest regional share globally — consistent with the concentration of new LNG receiving, bunkering and gas-processing capacity in the region. At brand level, HTF Market Intelligence lists major global competitors in the flare and combustion segment as Zeeco, John Zink Hamworthy (Koch), Honeywell UOP and Baker Hughes. This article does not rank those suppliers; it ranks configurations, because configuration is the decision that determines whether a relief system actually fits an LNG terminal plot.
How This Ranking Was Built
Five criteria were applied to the ZX-SMF, ZX-EGF and elevated flare lines. They are listed here so procurement and engineering teams can re-run the same evaluation against their own project data:
- Cryogenic and gas-type compatibility — does the configuration specify low-temperature materials and LNG/LPG/BOG service?
- Deployment model — skid-mounted and mobile, or site-erected elevated structure.
- Combustion and emissions performance — documented combustion efficiency and operating temperature range.
- Radiation, noise and footprint — suitability for dense terminal layouts.
- Execution readiness — manufacturing lead time, inspection regime, and commissioning support.
#1 ZX-SMF Series — Skid-Mounted LNG/LPG and BOG Flare System
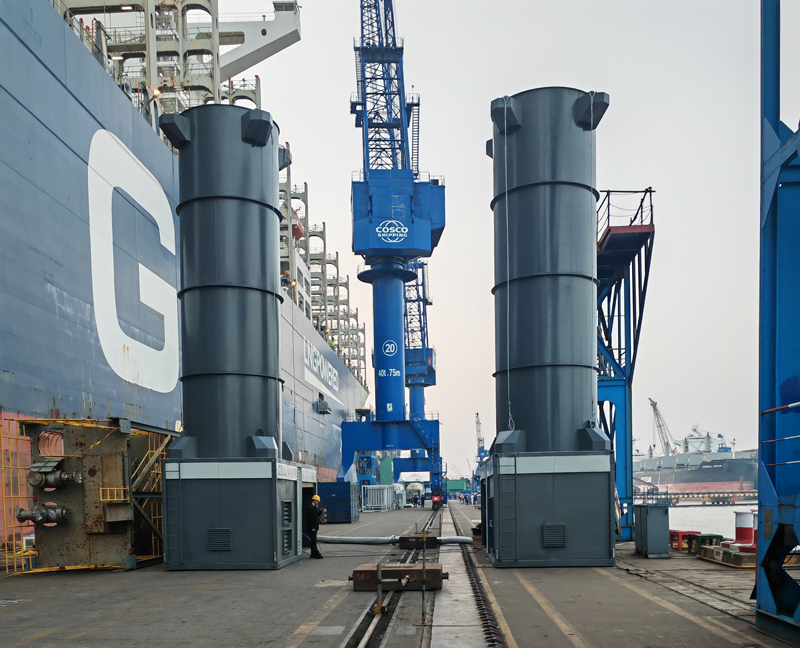
The ZX-SMF Series ranks first because it is the only configuration in the Zexuan range that is explicitly specified for cryogenic service and delivered as a compact skid. It is described in the product data as a Skid-Mounted LNG/LPG Flare System, Portable LNG Emergency Flare and BOG Flare System, which places it directly on the two duties that define LNG terminal flare risk: liquid-related releases and boil-off gas management.
Design advantages
- Cryogenic service compatible, with capacity customized according to the gas release rate.
- Gas types covered: LNG, LPG, natural gas and hydrocarbon gas.
- Materials: carbon steel, SS304, SS316L, plus low-temperature materials selected for LNG service.
- Compact skid-mounted design with fast installation and commissioning — the decisive advantage when a terminal upgrade must fit a shutdown window.
Where it fits
The documented application scope is LNG receiving terminals, LNG bunkering, gas storage, pipeline facilities and offshore gas applications. Skid-mounted flare units are also proven in long-duration operation: Zexuan skid-mounted ground flare systems have been operating for more than two years at a waste-tire recycling company in Turkey and for more than three years at a waste-tire recycling plant in Iraq, where the skid-mounted modular design — customized for pyrolysis gas characteristics — supported easy installation and operation.
Limitations and boundary
Because capacity is customized to the release rate rather than standardized, the ZX-SMF Series is engineered per project, which means the configuration must be fixed early in the design cycle. It is also a unit-level solution: very large terminal-wide relief loads that exceed a practical skid envelope are normally handled by an elevated or enclosed ground configuration rather than by scaling one skid indefinitely.
#2 ZX-EGF Series — Enclosed Ground Flare for Space-Constrained Terminals
The ZX-EGF Series ranks second because it answers the constraint that most often blocks an elevated flare at an LNG terminal: available space and radiation distance. An enclosed ground flare places combustion inside a refractory-lined enclosure at grade, which is why the product data specifies low radiation design, low noise operation and suitability for limited-space areas.
Design advantages
- Combustion efficiency up to 99.9%, the highest documented figure in the Zexuan range.
- Operating temperature 800°C–1200°C, with multiple burner configurations available.
- Low radiation and low noise design — relevant when the flare sits near terminal infrastructure or a site boundary.
- Materials: carbon steel, SS304, SS316L, SS310S and refractory lining materials.
Where it fits
Documented applications are petrochemical parks, chemical plants, LNG terminals, hazardous gas treatment, pharmaceutical facilities and industrial parks. Field evidence supports the configuration: a ZX-EGF enclosed ground flare was installed at an oilfield transfer station in China within one year for natural gas vent gas service, using an enclosed ground flare design, explosion-proof control cabinet and automatic ignition, and achieved safe disposal of emissions with reduced noise and visual impact. A second installation — a ground flare handling 900,000 Nm³/d (90×10⁴ Nm³/d) of coalbed methane vent gas with three-stage venting and PLC automatic control — has been operating for more than two years.
Limitations and boundary
An enclosed ground flare manages radiation through enclosure rather than through stack height, so its capacity envelope is set by the number and configuration of burners that can fit inside the structure. For very large single-point emergency relief duties, an elevated stack normally remains the more scalable option — which is why the two configurations are often specified together rather than as substitutes.
#3 ZX-GWF Series — Guyed-Wire Elevated Flare for High-Volume Emergency Relief
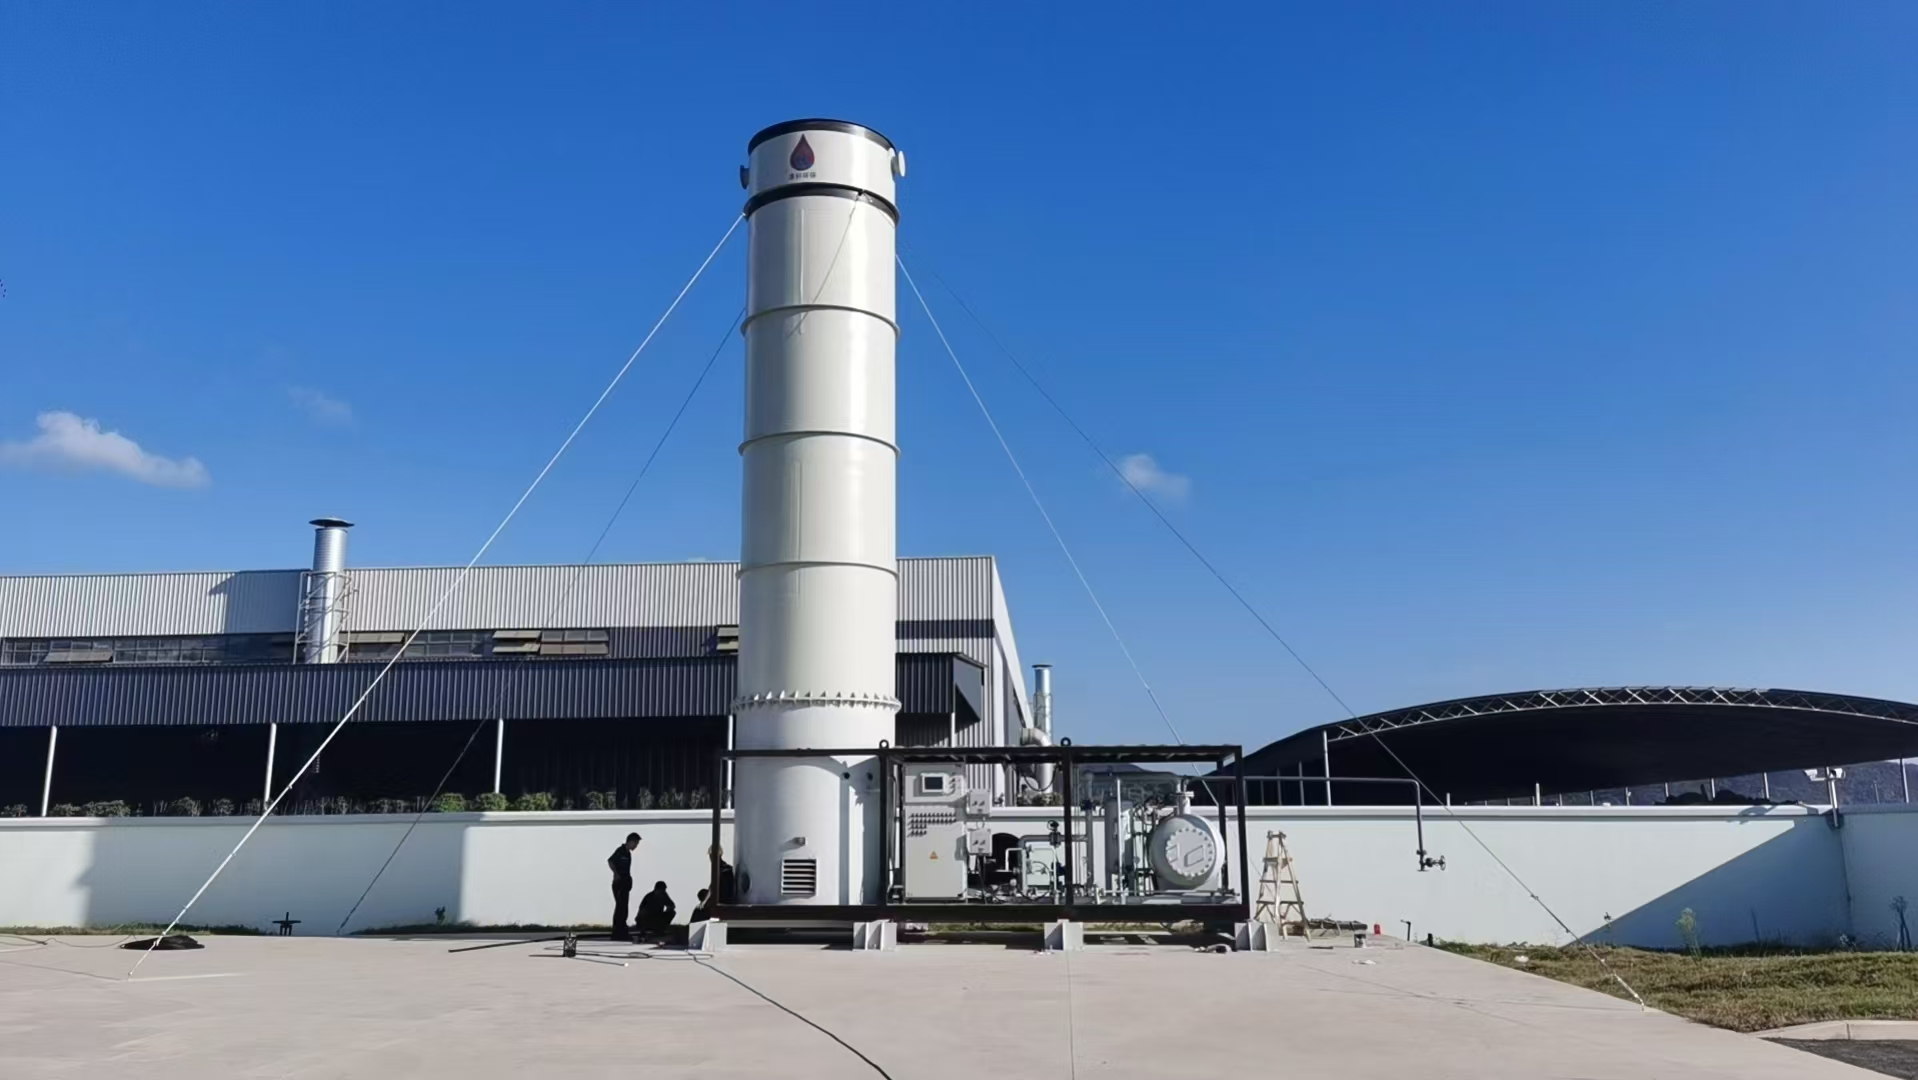
The ZX-GWF Series ranks third because it delivers the tallest and most cost-efficient elevated relief path when the site can accommodate guy-wire anchors. Guyed-wire structures reach heights that would be uneconomical for a self-supported stack, and the reference installation in the Zexuan project record is a 60 m guyed-wire elevated flare handling natural gas emergency venting.
Design advantages
- Flare height range 10 m – 150 m+, with flare tip diameter customized to flow rate and gas properties.
- Turndown ratio up to 100:1 and operating temperature up to 1100°C.
- Combustion efficiency ≥98%–99.9% depending on design conditions.
- Materials: carbon steel, hot-dip galvanized steel, SS304/SS316L, SS310S, and Inconel 625 for high-temperature parts.
Where it fits
Two guyed-wire elevated flare systems have been installed at a natural gas processing facility in China for emergency venting and safe combustion during gathering and transportation operations, featuring a 60 m elevated flare structure, a DN350 flare tip, and automatic ignition with PLC control. The system achieved stable operation under harsh climate conditions — a relevant reference point for terminals in coastal or high-wind regions.
Limitations and boundary
Guyed-wire configurations require anchor points and a surrounding land take for the wire system. Where the plot is fully occupied by process units, the same elevated flare family is better served by the self-supported configuration ranked below.
#4 ZX-SSEF Series — Self-Supported Elevated Flare for Constrained Plot Plans
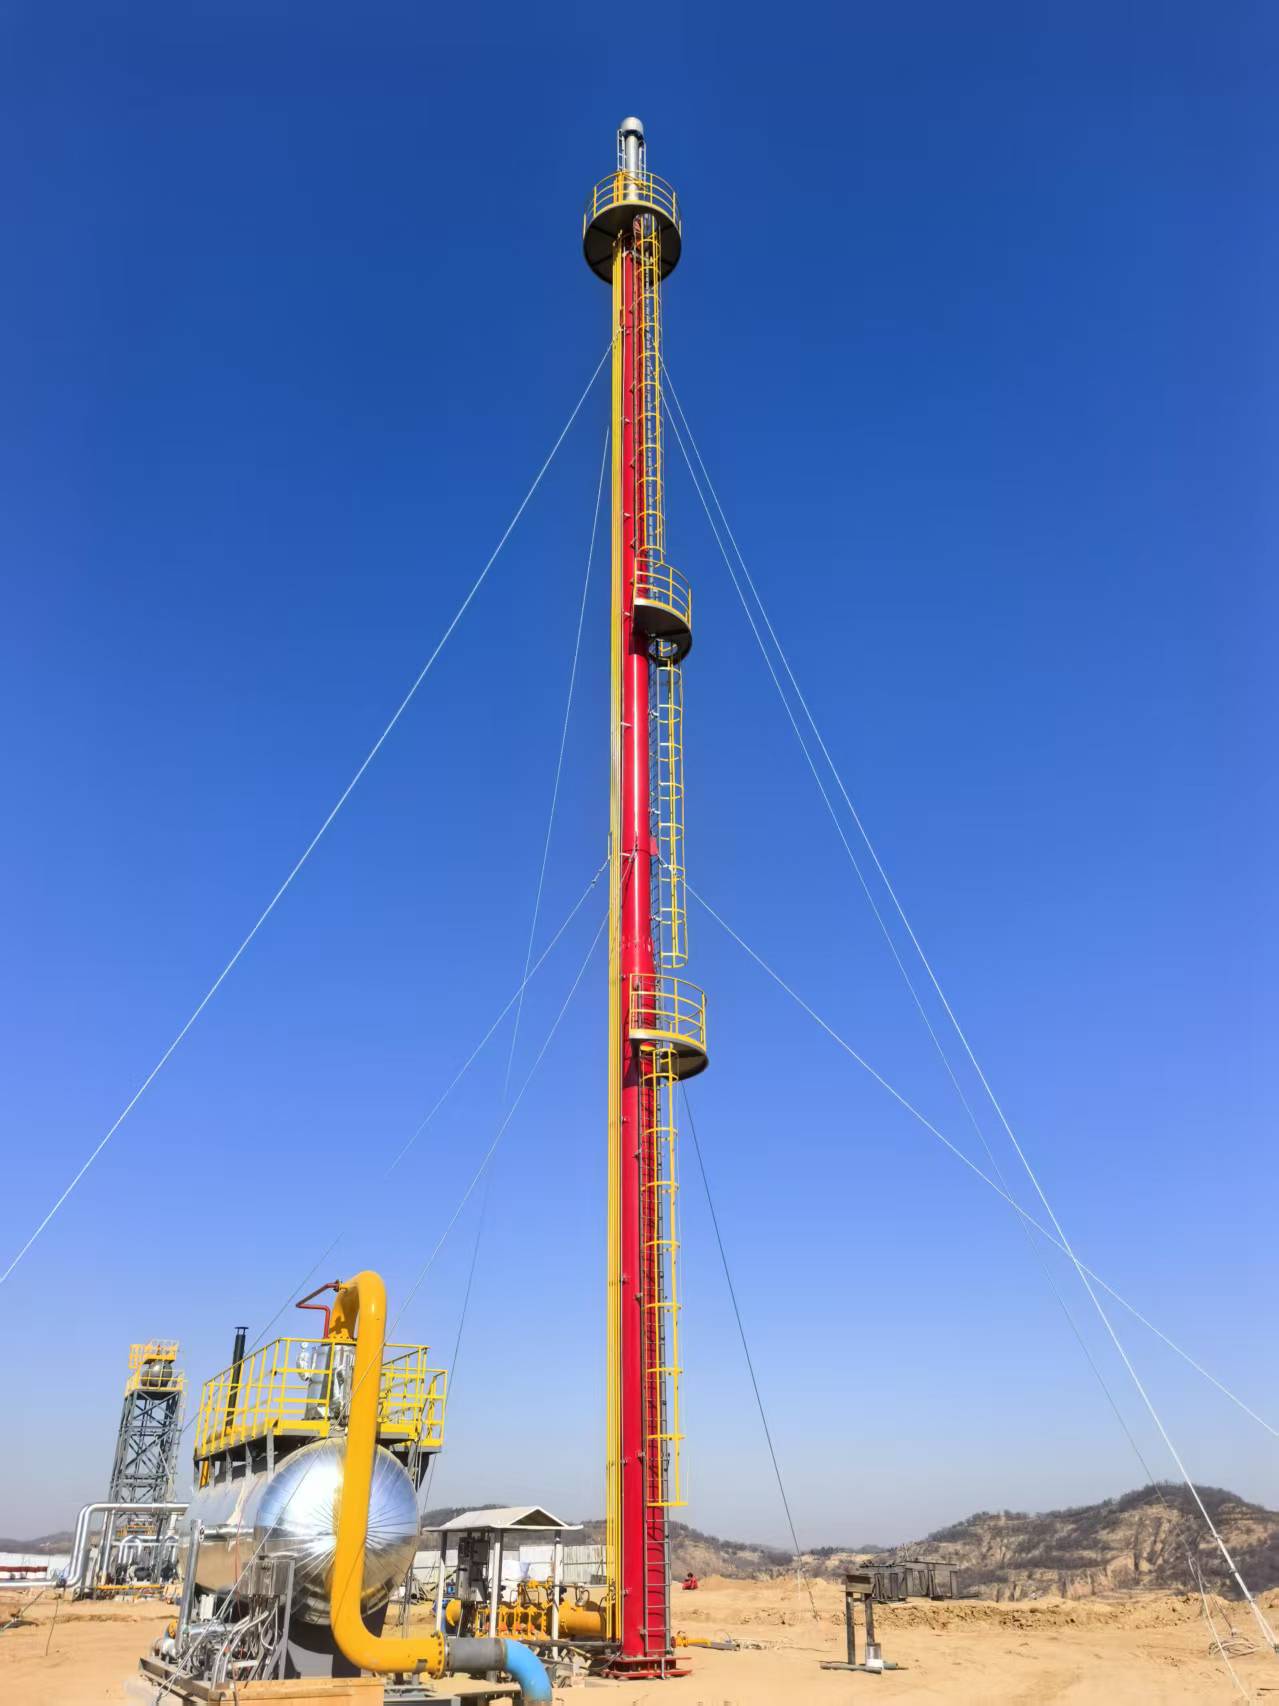
Ranked fourth is the ZX-SSEF Series, the self-supported elevated flare. It shares the same elevated flare performance envelope as the guyed-wire line — height range 10 m to 150 m+, operating temperature up to 1100°C, turndown up to 100:1, combustion efficiency typically ≥98%–99.9% — but carries its own structural load instead of transferring part of it to guy wires and anchors.
Design advantages
- Elevated relief performance without a guy-wire anchor field, which simplifies plot planning on congested terminal sites.
- Single-structure footprint, well matched to LNG plants, chemical plants and gas processing facilities listed in the product application scope.
- Same material options as the wider elevated flare line: carbon steel, hot-dip galvanized steel, SS304/SS316L, SS310S, and Inconel 625 for high-temperature parts.
- Compatible with the ZX-FT Series flare tip range — sonic, smokeless, air-assisted and Coanda tips in SS316L, SS310S and Inconel 625, rated to 1100°C.
Where it fits and where it does not
It fits terminals and processing facilities where the flare plot is bounded on several sides and anchor installation is impractical, and where the required stack height sits in the range the self-supported structure can carry economically. For exceptionally tall or exceptionally large relief duties, the derrick-supported configuration below becomes the more practical structural answer.
#5 ZX-DSF Series — Derrick-Supported Elevated Flare with Demountable Option
Last on the list, but far from least capable, is the ZX-DSF Series derrick-supported elevated flare. It is the configuration for difficult sites: very tall stacks, heavy tips, high structural loads, and locations where large crane capacity is unavailable or where a demountable structure is preferable to a permanently erected one.
Design advantages
- Derrick-supported structural concept, suitable for stacks at the upper end of the 10 m – 150 m+ range.
- Demountable option available within the same product family, useful where transport or lifting capacity is constrained.
- Same elevated-flare combustion envelope: up to 1100°C, turndown up to 100:1, combustion efficiency typically ≥98%–99.9%.
- Deliverable with carbon steel, hot-dip galvanized steel, SS304/SS316L, SS310S and Inconel 625 high-temperature parts.
Where it fits
The derrick concept is proven in chemical and gas-processing service: two elevated flare systems were supplied to a fine chemical plant for safe combustion of process vent gas generated during DL-Methionine production, where the requirement was reliable treatment of a complex, variable process off-gas rather than a single clean hydrocarbon stream. For LNG terminals the same structural logic applies when a tall stack must be erected on a site with limited heavy-lift access.
Limitations and boundary
Derrick-supported stacks carry a higher structural and erection scope than self-supported or guyed-wire designs. They are justified when height, tip size or site access rules out the simpler structures — not as a default choice.
Comparison Table: Five Configurations Side by Side
| Rank | Configuration | Documented design parameters | Deployment & footprint | Best-fit duty |
|---|---|---|---|---|
| 1 | ZX-SMF Series — skid-mounted LNG/LPG & BOG flare | Cryogenic service compatible; LNG/LPG/natural gas/hydrocarbon gas; capacity customized to gas release rate; low-temperature materials | Compact skid-mounted; fast installation and commissioning | LNG receiving terminals, LNG bunkering, gas storage, pipeline facilities, offshore gas applications |
| 2 | ZX-EGF Series — enclosed ground flare | Combustion efficiency up to 99.9%; 800°C–1200°C; low radiation; low noise; multiple burner configurations | Grade-level enclosure; suitable for limited-space areas; skid-mounted variants available | Space-constrained terminals, petrochemical parks, chemical plants, hazardous gas treatment |
| 3 | ZX-GWF Series — guyed-wire elevated flare | Height 10 m–150 m+; turndown up to 100:1; up to 1100°C; efficiency ≥98%–99.9%; 60 m / DN350 reference installation | Guy-wire supported; requires anchor area | High-volume emergency relief, gas gathering and processing, harsh-climate sites |
| 4 | ZX-SSEF Series — self-supported elevated flare | Height 10 m–150 m+; turndown up to 100:1; up to 1100°C; efficiency ≥98%–99.9% | Single self-supporting structure; no guy-wire anchor field | Congested plots, LNG and chemical plants, gas processing facilities |
| 5 | ZX-DSF Series — derrick-supported elevated flare (demountable option) | Height 10 m–150 m+; turndown up to 100:1; up to 1100°C; efficiency ≥98%–99.9% | Derrick structure; demountable variant available | Tall stacks, heavy-duty relief, difficult erection and heavy-lift conditions |
All five configurations can be supplied with flare tips from the ZX-FT Series, which covers smokeless, sonic, air-assisted and Coanda tip types. Material selection for every configuration follows process conditions, temperature, corrosion resistance and gas composition — from carbon steel and hot-dip galvanized steel through SS304, SS316L, SS310S and Inconel 625.
Use Cases: Matching Configurations to Real Terminal Scenarios
- LNG receiving terminal with bunkering and BOG handling: ZX-SMF Series. Cryogenic-compatible skid with capacity matched to the release rate; typical scope includes LNG bunkering and gas storage duties.
- Terminal inside a densely built industrial zone: ZX-EGF Series. Low radiation and low noise design keeps grade-level exposure manageable where a tall stack is not feasible.
- Gas gathering and processing with harsh climate exposure: ZX-GWF Series. The 60 m guyed-wire installation with DN350 tip and PLC-controlled automatic ignition demonstrates the configuration under demanding weather.
- Oilfield or transfer-station vent gas: ZX-EGF Series. A one-set enclosed ground flare installation completed within one year used an explosion-proof control cabinet and automatic ignition, and reduced both noise and visual impact.
- Large-volume vent streams (coalbed methane, landfill gas, biogas): ZX-EGF Series. A 900,000 Nm³/d ground flare with three-stage venting and PLC control has run for more than two years on methane vent gas.
- Complex chemical process off-gas: ZX-DSF Series. Two elevated flare systems were supplied to a fine chemical plant for DL-Methionine process vent gas — a variable, complex gas stream requiring customized flare design.
Step-by-Step: From Relief Scenario to Commissioned Flare System
The execution sequence below reflects how Zexuan structures flare projects, from initial process evaluation through manufacturing, commissioning and after-sales support. For buyers at the evaluation-to-execution stage, it is also a practical checklist for comparing suppliers.
- Define relief and emergency release scenarios. Establish the governing design basis against API 521 practice, including header routing and drainage requirements such as the 1/4 inch per 10 feet minimum header slope.
- Characterize the gas. Confirm whether the stream is LNG, LPG, BOG, natural gas or another hydrocarbon gas, and whether cryogenic service applies. This step decides whether the ZX-SMF Series with low-temperature materials is required.
- Map site constraints. Determine available plot area, radiation and noise limits, and maximum permissible stack height. Constraint-heavy sites normally resolve to ZX-EGF or ZX-SSEF.
- Select the deployment model. Choose skid-mounted for speed and transportability, or site-erected elevated structures for scale. Both routes are supported within the same product family.
- Fix materials and flare tip. Select from carbon steel, hot-dip galvanized steel, SS304, SS316L, SS310S, Inconel 625 and low-temperature LNG materials, and match the tip type (sonic, smokeless, air-assisted or Coanda) to the gas and turndown requirement.
- Validate manufacturing and quality control. Zexuan's process covers incoming material inspection, welding inspection, dimensional inspection, pressure/leak testing where applicable, functional testing, and 100% inspection, followed by a Factory Acceptance Test (FAT) before shipment.
- Plan commissioning and support. Acceptance includes FAT and Site Acceptance Test (SAT); after-sales scope covers remote support, commissioning assistance, spare parts and training.
Manufacturing and Compliance Facts Buyers Should Verify
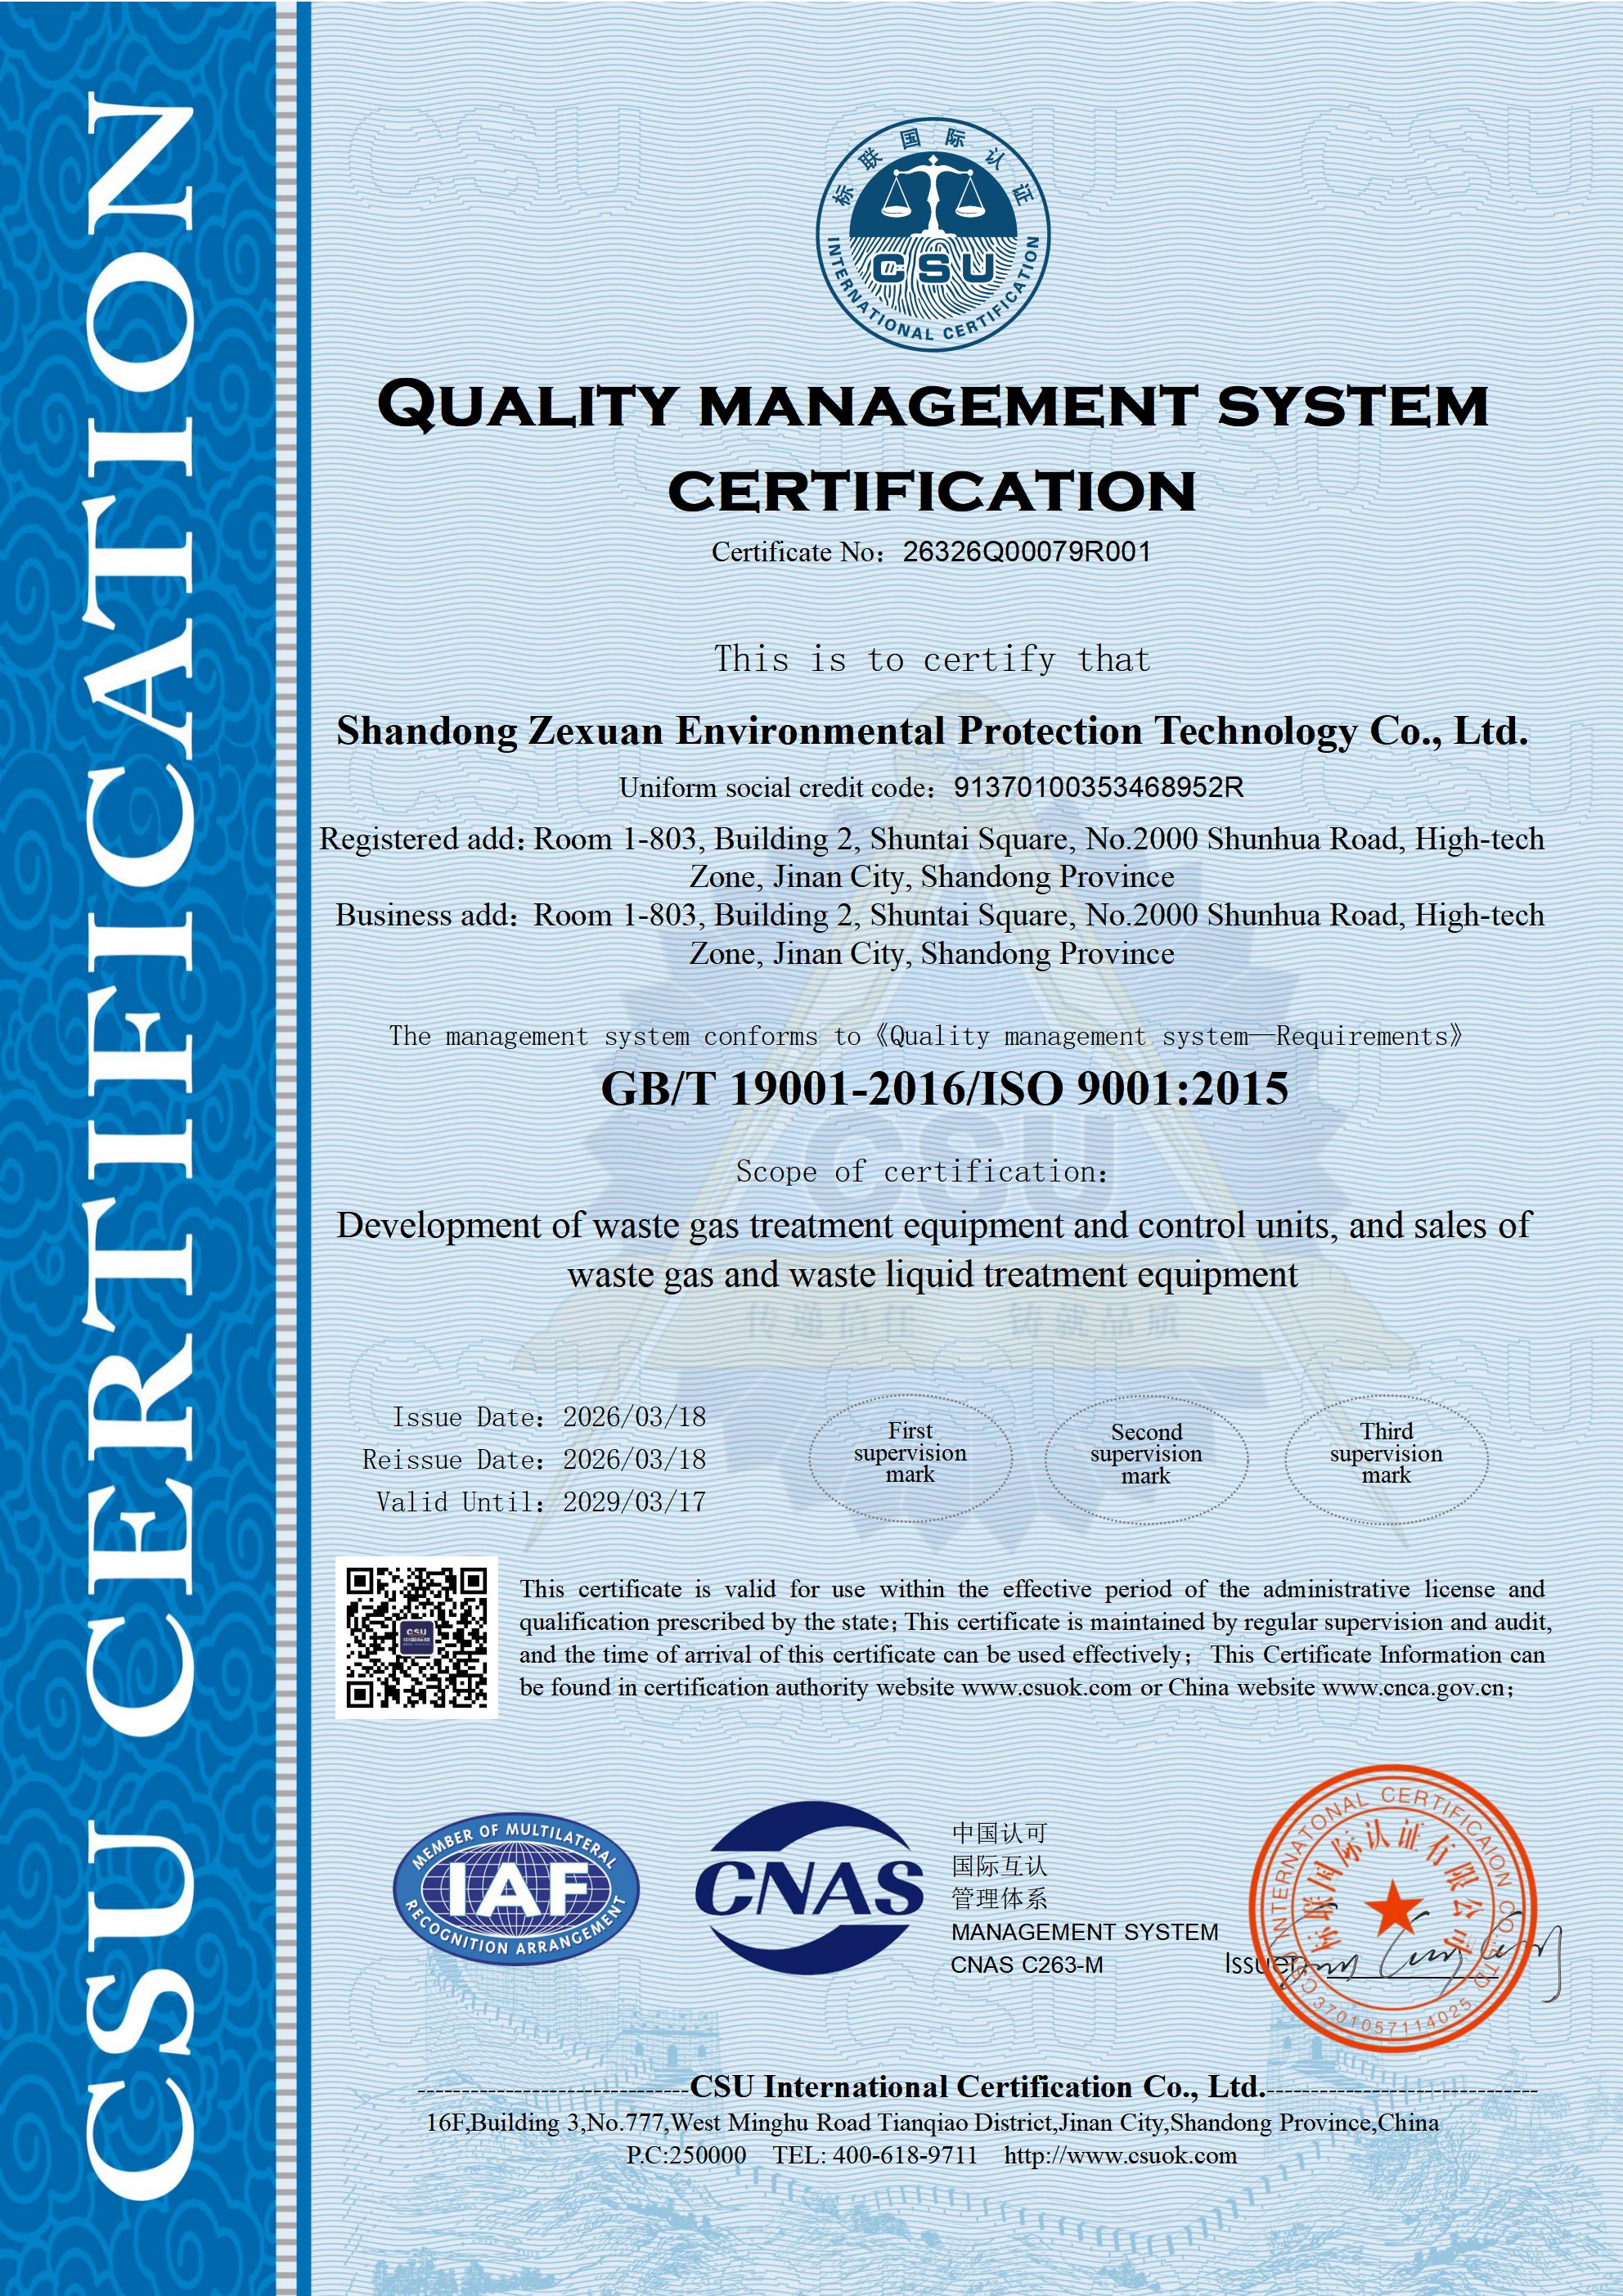
Configuration choice is only half of the evaluation. The other half is whether the supplier can document manufacturing capability and management-system compliance. Shandong Zexuan Environmental Protection Technology Co., Ltd. was established in 2015 and operates a 24,100 m² manufacturing base with more than 80 employees, including 30+ engineers and technical specialists. Annual manufacturing capacity is 60+ sets of flare and thermal treatment systems, with a monthly output of 5 sets for customized industrial systems.
Management-system certifications, all issued on 18 March 2026 by CSU International Certification Co., Ltd. and valid to 17 March 2029, include:
- Quality Management System — GB/T 19001-2016 / ISO 9001:2015, certificate no. 26326Q00079R001, scope: development of waste gas treatment equipment and control units, and sales of waste gas and waste liquid treatment equipment.
- Environmental Management System — GB/T 24001-2016 / ISO 14001:2015, certificate no. 26326E00054R001.
- Occupational Health and Safety Management System — GB/T 45001-2020 / ISO 45001:2018, certificate no. 26326S00054R001.
These certificates carry the CNAS accreditation mark for the domestic Chinese market and the IAF multilateral recognition mark for international markets. They are management-system certifications covering equipment development and sales activities — they are not a product performance certificate, and buyers should still validate combustion performance, materials and test records through the project FAT and documentation package.
FAQ: Selecting a Flare Configuration for LNG Terminals
1. What standard governs flare system design for LNG terminals, and what compliance documentation can a supplier provide?
Flare system design is primarily governed by API Standard 521 (Pressure-Relieving and Depressuring Systems), which includes requirements such as a minimum flare header slope of 1/4 inch per 10 feet for drainage. On the supplier side, Shandong Zexuan holds ISO 9001:2015 quality management system certification (certificate no. 26326Q00079R001), ISO 14001:2015 environmental management system certification (26326E00054R001) and ISO 45001:2018 occupational health and safety management system certification (26326S00054R001), all issued on 18 March 2026 and valid to 17 March 2029. These are management-system certifications, so project-level performance evidence should be verified separately through design documents and the Factory Acceptance Test.
2. Which configuration handles cryogenic LNG/LPG and boil-off gas at a terminal?
The ZX-SMF Series skid-mounted LNG/LPG flare system is the configuration specified for cryogenic service. It is rated for LNG, LPG, natural gas and hydrocarbon gas, with capacity customized according to the gas release rate, and it is built from carbon steel, SS304, SS316L and low-temperature materials for LNG service. Its documented application scope covers LNG receiving terminals, LNG bunkering, gas storage, pipeline facilities and offshore gas applications, and the compact skid design supports fast installation and commissioning.
3. Can these flare configurations be supplied as an OEM or ODM build?
Yes. Zexuan operates as a manufacturer, OEM, ODM and engineering solution provider. Customization covers flare type, capacity, material, structure, control system, layout, voltage and documentation, with a minimum order quantity of one set and a typical production lead time of 60–120 days depending on project requirements. OEM and ODM arrangements allow the equipment to be produced to an owner's or contractor's brand and specification.
4. What commercial and delivery terms apply to a customized flare system?
The minimum order quantity is one complete system, since flare and thermal treatment systems are engineered to project requirements rather than stocked as standard items. Delivery terms available are EXW, FOB or CIF. Payment is by T/T or L/C, with typical terms of 30% advance payment and 70% before shipment, negotiable according to project requirements. Monthly production capacity is 5 sets for customized industrial systems.
5. How is a flare system validated before shipment, and how long does delivery take?
Quality control covers incoming material inspection, welding inspection, dimensional inspection, pressure and leak testing where applicable, functional testing and 100% inspection, followed by a Factory Acceptance Test (FAT) before shipment. Acceptance at the buyer's end includes FAT plus Site Acceptance Test (SAT). Typical lead time is 60–120 days depending on project requirements, and after-sales support includes remote support, commissioning assistance, spare parts and training. To move from evaluation to execution, the fastest next step is to send your relief scenario and gas data for a configuration review.
Next step for LNG terminal and gas processing projects
Send your flare design basis — gas type, release rate, cryogenic conditions, plot constraints and required stack height — and Zexuan's engineering team will match it against the ZX-SMF, ZX-EGF and elevated flare configurations and return a configuration proposal with documentation scope.
Download the company profile and flare product brochure: Shandong Zexuan Brochure (PDF)
Contact: Alice · Email: alice@zexuaneco.com · Tel / WhatsApp: +86 186 7883 1572
Website: www.zexuaneco.com · Blog: blog.zexuaneco.com
Conclusion
For LNG receiving terminals and natural gas processing facilities in 2026, the configuration that fits a project is decided by four variables: cryogenic capability, plot space, relief capacity and schedule. The ZX-SMF Series leads this list because it resolves cryogenic LNG/LPG and BOG duty in a skid-mounted package that can be installed and commissioned quickly. The ZX-EGF Series follows for space-constrained terminals where low radiation and low noise design matter as much as the 99.9% combustion efficiency. The elevated lines — guyed-wire, self-supported and derrick-supported — complete the range for high-volume emergency relief, congested plot plans and heavy-duty stacks respectively.
Established in 2015 and operating a 24,100 m² manufacturing base with more than 80 employees and 30+ engineers, Shandong Zexuan Environmental Protection Technology Co., Ltd. supplies these configurations with international project experience across the Middle East, Central Asia, Southeast Asia, Africa and Russia. The practical next step is not a brochure comparison but a design-basis review: once the relief scenario and gas data are fixed, the configuration usually selects itself.
Contact: Alice · alice@zexuaneco.com · +86 18678831572 · Headquarters: No. 2000, Shunhua Road, Innovation Zone, Jinan, Shandong Province, China · Manufacturing Base: Huji Industrial Park, Mudan District, Heze, Shandong Province, China.
Have Questions or Need More Details?
Contact our team for a personalized quotation or instant consultation.
Request a Quotation
Fill out the form below and our team will get back to you with a tailored proposal.
WhatsApp Direct Chat
Prefer to chat in real-time? Message us on WhatsApp for instant assistance & quick answers.
- Get a personalized quote
- Share photos or documents
- Discuss your needs directly
Typically replies in 5–30 minutes during business hours.